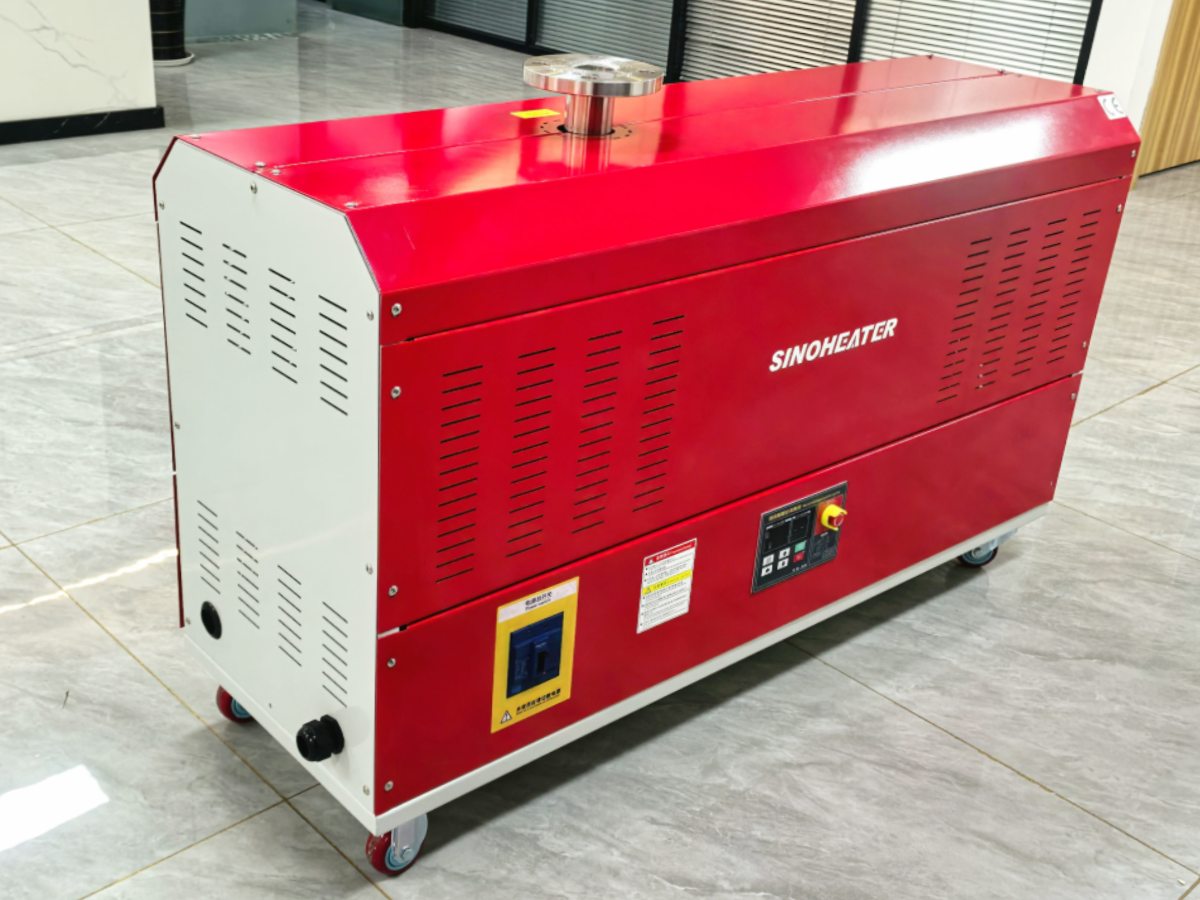
Hot air blower processing for plastic parts heat shrink packaging is a widely used industrial workflow that applies controlled, uniform high-temperature airflow to activate shrink films and create a tight, secure wrap around finished components. This method delivers consistent, gentle heat distribution that conforms closely to complex part geometries, making it suitable for everything from small precision plastic components to larger assembled units that need tamper-evident, dust-resistant outer packaging. When configured and executed correctly, this process creates a clean, professional finish that protects parts from surface scratches, dust contamination, and minor moisture exposure during storage and transit.
Pre-processing preparation for stable shrink results
Before starting the heat shrink workflow, confirm that all plastic parts are fully clean, dry, and free of residual surface oil or loose debris that could get trapped between the part and the shrink film during processing. Select a shrink film material that is compatible with the specific plastic part’s maximum heat tolerance, so the applied processing temperature will not cause warping, surface discoloration, or dimensional deformation of the component underneath. Position each part inside the pre-cut shrink sleeve or wrap with enough uniform clearance around all edges, to ensure the film has room to shrink evenly without pulling tight against sharp corners and creating unwanted tears. Arrange the work area in a well-ventilated space with no nearby flammable materials, and make sure the hot air blower airflow path will never be pointed directly at any unprotected skin or sensitive surrounding equipment.
Controlled heat application techniques for uniform wrapping
Start applying hot air at a moderate working distance from the shrink film, moving the airflow in slow, continuous sweeping motions across the entire surface of the wrapped part instead of holding the heat fixed on one single spot. Begin heating from the outer edges of the film and work gradually inwards, so the material shrinks evenly and releases trapped air smoothly without forming unsightly bubbles or localized wrinkles. For parts with complex contours, deep grooves, or protruding features, adjust the angle of the airflow to target recessed areas first, making sure the film pulls fully down into every gap before the outer surfaces finish shrinking. Keep the part rotating slowly or reposition it manually as you work, so no single section of the film or the underlying plastic part is exposed to excessive heat for too long.
Post-processing cooling and quality validation steps
Once the shrink film has pulled fully tight and conformed to every shape of the plastic part, move the wrapped unit away from the hot air flow immediately to let it cool down at room temperature in open, circulating air. Avoid touching or adjusting the film while it is still hot and slightly flexible, as this can leave permanent indentations, shifts, or uneven marks on the finished packaging surface. After the unit has fully cooled, perform a quick visual check across the entire wrap to confirm there are no tears, weak spots, or loose areas that could compromise the protective seal. For high-volume continuous processing, spot check a sample of finished units at regular intervals to confirm the heat application technique is staying consistent, and make small adjustments to airflow speed or working distance if you notice any new signs of uneven shrinking or part overheating.