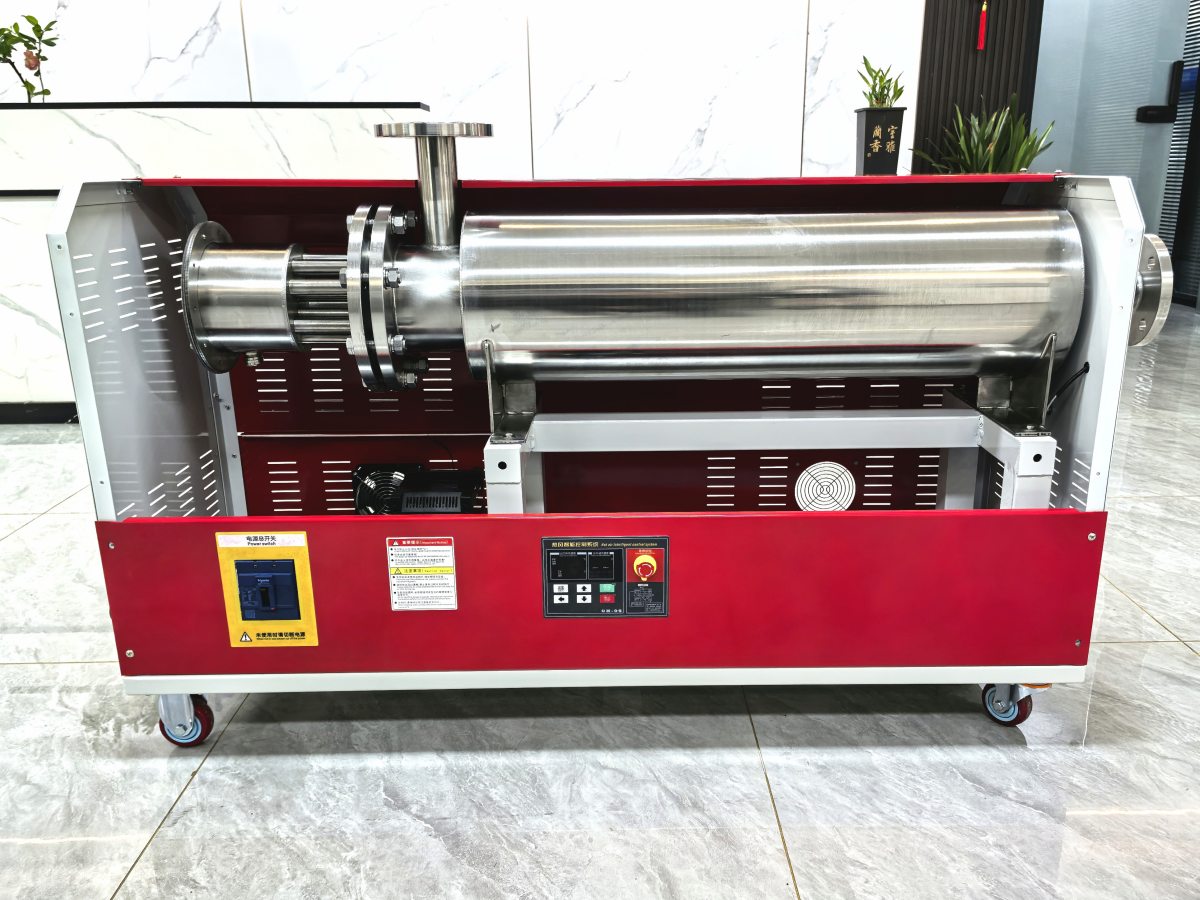
Hot air drying is one of the most widely used, reliable processes for curing paint coatings on hardware workpieces across industrial finishing workshops. When set up and operated correctly, it delivers consistent, uniform drying results that eliminate common defects like uneven film formation, trapped solvent bubbles, and surface tackiness that often appear with ambient air curing. Mastering the core operating principles and practical workflow details helps teams achieve high-quality, repeatable finishing results for every batch of hardware parts.
Pre-Drying Workpiece Preparation and Paint Film Pre-Inspection
Before introducing any hot air to the freshly painted hardware workpieces, complete a full pre-inspection step to confirm every part meets the required baseline conditions for successful drying. Check that the wet paint film thickness is consistent across all surfaces of each workpiece, with no areas of excessive buildup that would trap large volumes of solvent deep inside the coating. Uneven film thickness is one of the most common root causes of blistering, bubbling, or incomplete curing when hot air is first applied.
Arrange all workpieces on dedicated racks that keep every surface fully exposed to circulating air, with no overlapping sections or points where two parts touch each other. Ensure there is at least 5cm of open space between every individual part, so hot air can flow freely around the entire workpiece, including hidden edges, threaded holes, and recessed crevices that are easily missed in poorly arranged batches. Even small blocked sections will create uneven drying that leaves sticky uncured spots on the final finish.
Let the freshly painted workpieces sit at stable room temperature for a short flash-off period before applying any heated air. This initial rest time lets the largest portion of volatile solvent evaporate slowly and evenly at low temperature, before you raise the ambient air temperature. Skipping this flash-off step and applying high heat immediately will cause the outer surface of the wet paint to skin over rapidly, trapping solvent underneath that can never fully escape, leading to permanent bubbling and delamination defects.
Hot Air Temperature Ramp and Gradient Control
The drying process must follow a carefully staged, gradual temperature rising sequence, rather than jumping directly to maximum target temperature the moment workpieces enter the drying zone. Start the cycle at a relatively low initial air temperature that is only slightly higher than ambient room conditions, then raise the temperature in small, steady increments over a predefined period. This slow ramp gives solvent trapped deep inside the paint film time to escape gradually, without creating rapid vapor bubbles that break through the wet surface.
Set the peak drying temperature to a level that matches the specific paint formulation and the base material properties of the hardware workpiece. For thin, easily heat-deformed metal parts, keep peak temperatures low enough to avoid thermal warping that would ruin the dimensional tolerance of precision components. For thicker, more thermally stable hardware, you can use a higher peak temperature to speed up full cross-linking of the paint binder and reduce total cycle time.
Maintain a completely uniform temperature distribution across the entire drying zone, with no localized hot spots that run more than 5°C above the set target value. Hot spots cause the paint film in those areas to cure far faster than surrounding sections, creating uneven gloss levels, different color tones, and internal thermal stress that makes the coating far more prone to cracking or peeling long after the parts leave the workshop. Use multiple distributed temperature sensors across the full drying space to monitor and adjust for consistent heat distribution.
Airflow Velocity and Circulation Pattern Optimization
The speed and direction of circulating hot air plays a critical role in removing solvent vapor from the surface of the wet paint without damaging the soft, uncured film. Set initial airflow velocity during the early low-temperature phase low enough to avoid creating visible ripples, streaks, or flow marks on the soft wet paint surface. As the paint film gradually cures and gains mechanical strength later in the cycle, you can increase airflow velocity slightly to carry away remaining solvent vapor more efficiently.
Design the circulation pattern to move fresh hot air directly across the surface of every workpiece, rather than just circulating it in open empty space above the racks. Direct a portion of the airflow toward the small gaps and recessed features on each hardware part, where trapped solvent vapor tends to accumulate and linger. This prevents stagnant pockets of high solvent concentration from forming right above the paint surface, which would slow down evaporation and leave behind uneven drying defects.
Install dedicated exhaust vents at the opposite end of the drying zone from the fresh hot air intake, to continuously pull away solvent-saturated moist air and replace it with fresh, low-humidity heated air. Never let the same air recirculate indefinitely without venting, because as solvent concentration in the air rises, the evaporation rate from the paint film slows down drastically, extending total required drying time and leading to incomplete curing.
Post-Drying Cool Down and Final Curing Validation
Once the full high-temperature drying cycle is complete, do not pull the hot hardware workpieces out into cool ambient open air immediately for rapid cooling. A sudden extreme temperature shock can create thermal stress between the metal base material and the hardened paint film, leading to fine invisible cracking that only becomes visible weeks or months later. Instead, let the parts cool down gradually inside the drying zone as the air temperature slowly drops back to room temperature over an extended period.
After the workpieces reach full ambient temperature, perform a set of simple validation checks to confirm the paint film has achieved full, uniform curing. Gently press a clean finger against a hidden non-critical edge of the coating to confirm no surface tackiness remains, and perform a light rub test with a clean dry cloth to confirm no soft uncured paint transfers onto the fabric. Check all hidden edges, threaded sections, and recessed areas specifically, as these are the locations most likely to retain residual uncured material.
Document every key parameter for each drying batch, including total cycle time, temperature ramp profile, average airflow velocity, and peak temperature reading. This historical dataset lets you refine and standardize the process for different types of hardware workpieces and different paint formulations over time, building up a proven, repeatable workflow that delivers consistent high-quality finishing results for every production run.