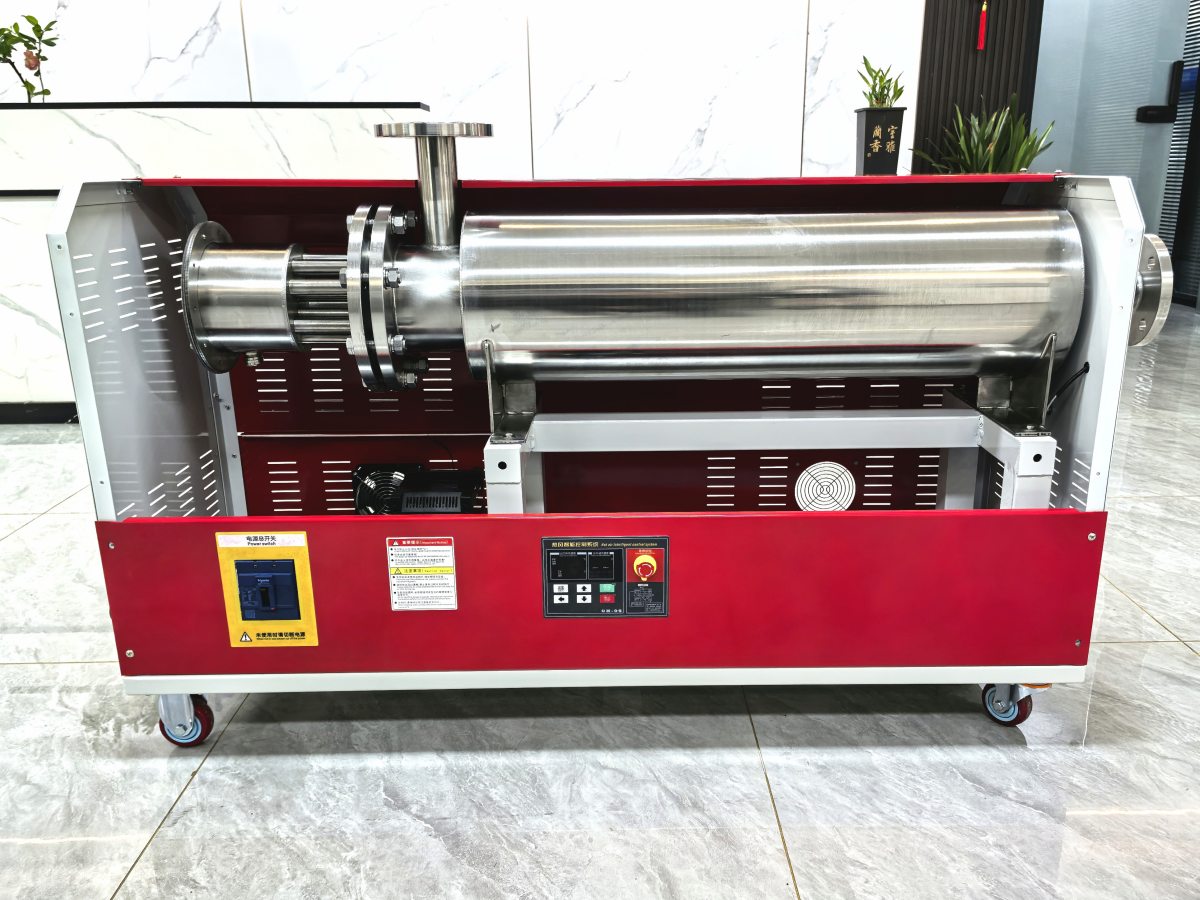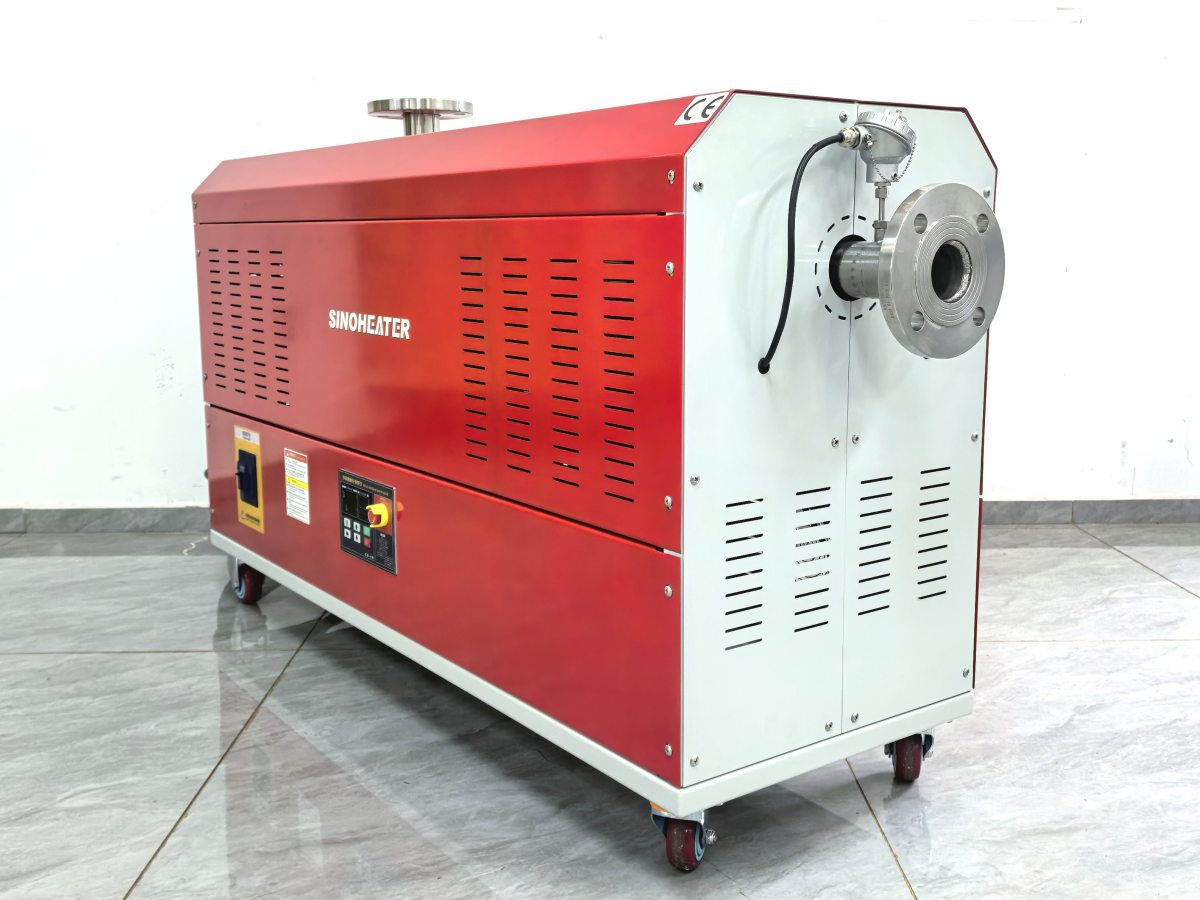
Hot air heating is a widely adopted, highly reliable process for secondary shaping of rubber products in industrial production workflows. Unlike direct contact heating methods that can easily create localized overheating and surface scorching, circulating hot air delivers even, consistent thermal energy across every surface of the workpiece, supporting precise, controllable deformation and reshaping without damaging the intrinsic material properties of the rubber. Mastering the core operational details of this process helps production teams achieve highly repeatable shaping results while minimizing scrap rates.
Pre-Heating Workpiece Condition and Pre-Processing Setup
Before introducing any heated air to the rubber workpieces, perform a full inspection to confirm every part meets the required baseline conditions for stable secondary shaping. Check that all raw rubber parts have been properly stored in a temperature-stable environment for at least 12 hours before processing, so their internal material temperature is completely consistent and matches ambient room conditions. Workpieces with uneven internal temperatures will absorb heat at different rates during processing, leading to inconsistent deformation that cannot be controlled accurately.
Remove all traces of residual release agent, surface dust, or leftover processing oil from the surface of every rubber part before placing them in the heating zone. Any foreign contamination on the rubber surface will act as an insulating barrier, disrupting uniform heat transfer and creating localized cold spots that prevent full, even softening of the material across the entire workpiece. This small pre-cleaning step eliminates a huge percentage of common uneven shaping defects.
Arrange the workpieces on open mesh racks that support every part without blocking any major surface, leaving sufficient open space between individual pieces to let hot air flow freely around all sides, including internal hollow cavities and narrow gaps in complex profile parts. No two rubber pieces should be touching each other at any point during the heating cycle, as contact points will trap heat unevenly and create unwanted localized sticking or over-softening.
Hot Air Temperature Profiling and Gradient Control
The heating sequence for secondary rubber shaping must follow a carefully calibrated, gradual temperature rising profile, rather than exposing the workpieces directly to the maximum target temperature in one sudden step. Start the cycle at a moderate initial temperature well below the material’s softening point, holding this level for a set period to ensure the entire mass of the rubber part reaches a uniform baseline temperature all the way through its cross-section. This eliminates the common problem where the outer surface of the rubber softens too quickly while the inner core remains cold and rigid.
Raise the temperature in small, controlled increments until you reach the exact target heating temperature matched to the specific rubber compound being processed. For most common formulations, this temperature sits well below the material’s primary curing temperature, high enough to soften the rubber network for controlled plastic deformation but low enough to prevent unintended additional cross-linking that would permanently alter the material’s final elasticity and hardness. Even a 10°C overshoot beyond this safe range can ruin the intrinsic physical properties of the finished part.
Maintain a perfectly uniform temperature distribution across every section of the heating chamber, with no localized hot spots that deviate more than 3°C from the set target. Hot spots will cause the rubber in those areas to over-soften, leading to sagging, surface blistering, or unintended permanent deformation that falls completely outside the required shaping tolerance. Use multiple evenly distributed temperature sensors to continuously monitor and adjust heat output to keep conditions fully consistent across the entire working zone.
Airflow Circulation and Uniform Heat Transfer Optimization
Design the hot air circulation pattern to move high-volume, low-velocity airflow evenly across every surface of the rubber workpieces. Avoid excessively high airflow speeds that can push softening thin-walled rubber parts out of shape before they are secured in their final shaping fixtures. The goal is to create continuous, gentle air movement that eliminates stagnant cold pockets and ensures every part receives exactly the same amount of thermal energy at every moment during the heating cycle.
For complex profile rubber parts with deep recesses, narrow channels, or hollow internal structures, direct a portion of the circulating airflow to flow directly through these hard-to-reach features. This ensures even the innermost surfaces receive consistent heat, preventing uneven softening that leaves hidden internal stress in the finished shaped part. Without this targeted airflow, internal cavities can remain far cooler than the outer surface, leading to springback and shape distortion after the part is removed from its fixture.
Maintain consistent low humidity levels in the circulating hot air stream by continuously venting a small portion of moist process air and replacing it with fresh, dry heated air. Excessively high humidity in the heating chamber creates a thin layer of condensation on the cool rubber surface at the start of the cycle, slowing down heat transfer and leaving faint water marks on the finished surface that are very hard to remove.
Post-Heating Transfer, Shaping and Controlled Cooling
As soon as the rubber workpieces reach their target uniform softening temperature, transfer them immediately and smoothly to the pre-prepared secondary shaping fixtures. Minimize the total transfer time to less than 10 seconds, so the rubber does not lose too much heat and start to stiffen before it is fully secured in the mold. Even a small drop in core temperature at this stage can create uneven resistance to deformation that leads to incomplete shape forming.
Once the parts are fully clamped and secured in their fixtures, run a controlled steady cooling cycle that brings the temperature down gradually back to ambient levels. Never use forced cold air or water quenching to speed up cooling, as rapid temperature change will create severe uneven thermal stress inside the rubber material, leading to significant springback, shape distortion, or hidden internal micro-cracks that appear weeks later in finished parts. Let the entire fixture and enclosed rubber part cool down together at a slow, consistent rate.
After the parts are fully cooled to room temperature and removed from the fixtures, perform a full dimensional check to confirm all key shaping dimensions fall within required tolerance. Document all key process parameters for the batch, including total heating time, peak temperature, average airflow speed, and full cooling cycle duration. This historical reference data lets you refine and standardize the process for different rubber compounds and part geometries over time, building a robust, repeatable workflow that delivers consistent, low-scrap results for every production run.